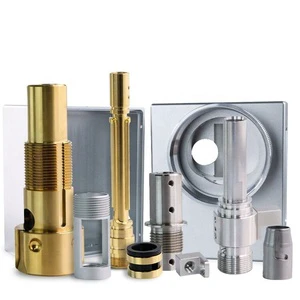
A Squeeze Casting Die works under heat and pressure, so the design problem is thermal: metal has to fill, freeze and release at a rate the cycle time depends on. Designed for LED lighting housings, this Squeeze Casting Die is produced in H13 tool steel and nitrided cavities with die design with flow simulation, EDM detail and thermal balancing. The figures below are the ones recorded at tryout rather than theoretical values.
Tolerance is applied where it does work rather than across the whole drawing. Critical features are held to cavity tolerance ±0.05 mm, non-critical dimensions follow the general machining tolerance, and the difference is stated in the quotation rather than discovered later.
Specification
| Process | Die design with flow simulation, edm detail and thermal balancing |
|---|---|
| Material / configuration | H13 tool steel and nitrided cavities |
| Size / capacity | cavity tolerance of ±0.05 mm |
| Tolerance | cavity tolerance ±0.05 mm |
| Surface finish | polished, nitrided or shot blasted cavity surfaces |
| Application | squeeze casting die for LED lighting housings |
| Inspection | Dimensional report, material certificate, first article report on request |
| Lead time | 7–15 working days for samples, 3–4 weeks for production |
| Minimum order | 1 piece for prototypes, from 50 pieces for production pricing |
Manufacturing process
Work is carried out with die design with flow simulation, EDM detail and thermal balancing. Tooling, speeds and fixturing are recorded with the part number, so a repeat order starts from a proven process instead of a fresh setup.
Material is purchased against a certificate and checked on receipt, so the composition is known before any cutting starts. Work in progress is identified by part number and operation, and the finished parts are deburred, cleaned and protected before they leave the machine area.
Typical applications
Most of the work supplied in this category falls into the following examples.
- Structural automotive brackets.
- Heat sink and lighting housings.
- Gear box and pump bodies.
- Consumer appliance frames.
- Electric motor housings.
Quality control and documentation
Critical features are measured on calibrated equipment in a controlled room, and the results are filed with the job so that a repeat order can be compared with the first.
Material certificates to EN 10204 3.1, dimensional reports and first article inspection reports are issued with the shipment where the application requires them. Calibration dates and measurement uncertainty are recorded alongside every result.
Ordering, lead time and packaging
Packaging is specified by the part: individual protection for finished surfaces, separation for assemblies, and export crating with a packing list for shipment.
Frequently asked questions
How is porosity controlled?
By gating and venting designed from flow simulation, plus vacuum assistance on structural parts. Impregnation is a repair, not a substitute for correct fill.
What die life should be expected?
Aluminium dies in H13 typically deliver 80,000 to 150,000 shots with scheduled maintenance. Zinc tools run longer because the melt temperature is far lower.
Can you supply material and inspection certificates?
Yes. Material certificates to EN 10204 3.1, full dimensional reports, first article inspection reports and, where required, PPAP or AS9102 documentation are issued with the shipment.
Drawings are reviewed for manufacturability before quotation, and any feature that adds cost without adding function is pointed out at that stage rather than after the parts are made.