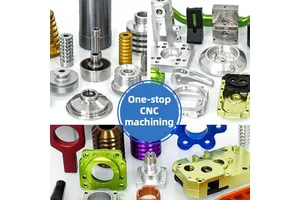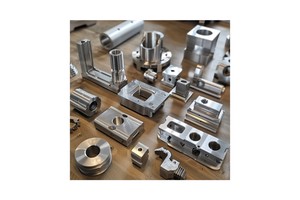
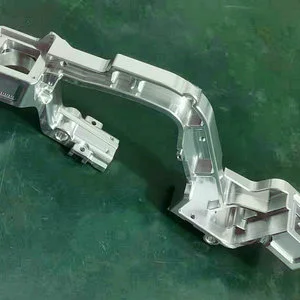
A CNC Milling Spare Parts Components Cnc removes material with a rotating cutter, producing pockets, slots, contours and three dimensional surfaces. Supplied to aerospace suppliers, this CNC Milling Spare Parts Components Cnc is configured with 6061-T6 aluminium. CNC milling with adaptive roughing and finish passes is carried out on equipment that holds ±0.02 mm across a full shift, not only on a first piece.
Tolerance is applied where it does work rather than across the whole drawing. Critical features are held to ±0.02 mm, non-critical dimensions follow the general machining tolerance, and the difference is stated in the quotation rather than discovered later.
Specification
| Process | Cnc milling with adaptive roughing and finish passes |
|---|---|
| Material / configuration | 6061-T6 aluminium |
| Size / capacity | pocket depth held within 0.05 mm |
| Tolerance | ±0.02 mm |
| Surface finish | milled finish, Ra 0.8–3.2 µm |
| Application | cnc milling spare parts components cnc for aerospace suppliers |
| Inspection | Dimensional report, material certificate, first article report on request |
| Lead time | 7–15 working days for samples, 3–4 weeks for production |
| Minimum order | 1 piece for prototypes, from 50 pieces for production pricing |
Manufacturing process
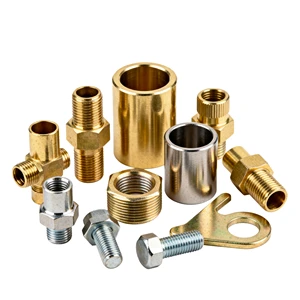
Work is carried out with CNC milling with adaptive roughing and finish passes. Tooling, speeds and fixturing are recorded with the part number, so a repeat order starts from a proven process instead of a fresh setup.
Material is purchased against a certificate and checked on receipt, so the composition is known before any cutting starts. Work in progress is identified by part number and operation, and the finished parts are deburred, cleaned and protected before they leave the machine area.
Typical applications
Most of the work supplied in this category falls into the following examples.
- Mould and die cavities.
- Machine base plates.
- Aerospace ribs and spars.
- Impeller and blisk roughing.
- Instrument panels and enclosures.
Quality control and documentation
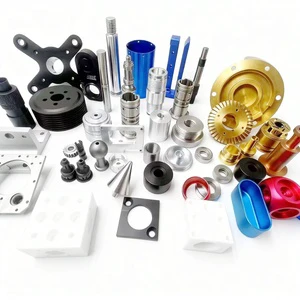
Critical features are measured on calibrated equipment in a controlled room, and the results are filed with the job so that a repeat order can be compared with the first.
Material certificates to EN 10204 3.1, dimensional reports and first article inspection reports are issued with the shipment where the application requires them. Calibration dates and measurement uncertainty are recorded alongside every result.
Ordering, lead time and packaging
Packaging is specified by the part: individual protection for finished surfaces, separation for assemblies, and export crating with a packing list for shipment.
Frequently asked questions
What is the difference between 3, 4 and 5 axis?
Three axis machines cut prismatic parts; a fourth rotates the part for features around a cylinder; five axis tilts the cutter or table so compound angles are reached in one setup.
How is surface finish controlled?
By the stepover, the cutter geometry and the final finishing pass. Ra 1.6 µm is routine, and Ra 0.8 µm is achieved with a fine stepover and a sharp, balanced tool.
Do you keep tooling and programmes for repeat orders?
Fixtures, tool lists and verified CAM programmes are retained for the life of the part number, so a repeat release runs on the same setup as the first batch without a new proving run.
Drawings are reviewed for manufacturability before quotation, and any feature that adds cost without adding function is pointed out at that stage rather than after the parts are made.