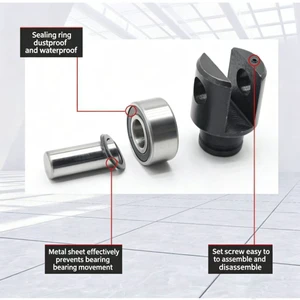
A Drill and Tap Centre is the general purpose workhorse of a machining workshop, configured to complete several operations in one clamping. The Drill and Tap Centre described here is built with a pallet changer and probing package and specified for tool and die shops. multi-axis CNC machining with probing and through-tool coolant sits behind the numbers below, which are stated as delivered rather than as a best case.
The parts that matter most are the interfaces: bores, sealing faces, threads and mounting patterns. Those are held to ±0.008 mm, verified against the drawing, and recorded before anything is packed.
Specification
| Process | Multi-axis cnc machining with probing and through-tool coolant |
|---|---|
| Material / configuration | a pallet changer and probing package |
| Size / capacity | 1000 × 600 × 600 mm travel |
| Tolerance | ±0.008 mm |
| Surface finish | machined finish, Ra 0.8–1.6 µm |
| Application | drill and tap centre for tool and die shops |
| Inspection | Dimensional report, material certificate, first article report on request |
| Lead time | 7–15 working days for samples, 3–4 weeks for production |
| Minimum order | 1 piece for prototypes, from 50 pieces for production pricing |
Manufacturing process
The operation sequence is decided before the first chip is cut: roughing to leave even stock, semi-finishing, then multi-axis CNC machining with probing and through-tool coolant as the final operation. That order is what keeps ±0.008 mm stable as the batch runs and the machine warms up.
Material is purchased against a certificate and checked on receipt, so the composition is known before any cutting starts. Work in progress is identified by part number and operation, and the finished parts are deburred, cleaned and protected before they leave the machine area.
Typical applications
Most of the work supplied in this category falls into the following examples.
- Housings and gearbox casings.
- Mould plates and inserts.
- Structural aerospace brackets.
- Manifolds and valve bodies.
- Jig and fixture bodies.
Quality control and documentation
Every batch is measured against the drawing with calibrated equipment, and results are recorded against the part number rather than kept on a scrap of paper.
Material certificates to EN 10204 3.1, dimensional reports and first article inspection reports are issued with the shipment where the application requires them. Calibration dates and measurement uncertainty are recorded alongside every result.
Ordering, lead time and packaging
Quotations are returned within one working day of a complete drawing package. Lead time is quoted from drawing approval, not from the date of enquiry.
Frequently asked questions
How many axes are needed?
Three axes cover prismatic parts. A fourth adds features around a cylinder and a fifth reaches compound angles and undercuts, removing setups and the tolerance stack that comes with them.
What does probing actually add?
Tool setting, datum finding and in-process measurement. Drift is corrected while there is still stock to remove, instead of being found at final inspection.
What file formats do you need for a quotation?
STEP or IGES for the 3D model and a PDF drawing with tolerances, material and surface finish called out. Native files from SolidWorks, Creo or Inventor are also accepted.
To discuss drill and tap centre requirements, send the model and the drawing with the quantities required. Feedback on manufacturability is given free of charge before any order is placed.