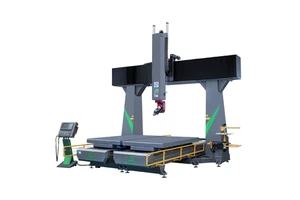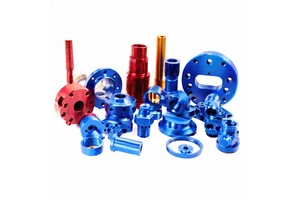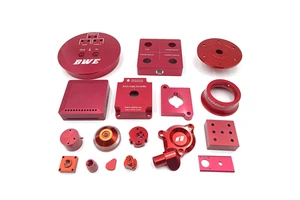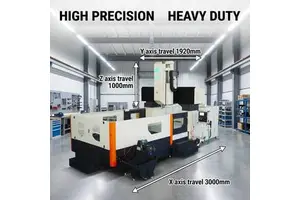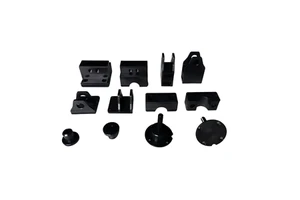
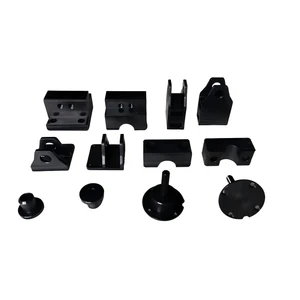
A Indexing Fixture moves setup work off the machine table and onto a bench, so the spindle keeps cutting while the next job is prepared. This page covers the Indexing Fixture configured with a pneumatic circuit with pressure sensing and supplied to high mix electronics machining: zero point clamping with modular workholding and tombstone fixtures. The headline figure is clamping forces to 25 kN, and the rest of the page explains what it means in daily use.
In practice the difficulty is rarely the nominal size. repeatability within 0.005 mm is held on the features that locate the part in the assembly, and the process is set up so that the first piece and the five hundredth measure the same way.
Specification
| Process | Zero point clamping with modular workholding and tombstone fixtures |
|---|---|
| Material / configuration | a pneumatic circuit with pressure sensing |
| Size / capacity | clamping forces to 25 kN |
| Tolerance | repeatability within 0.005 mm |
| Surface finish | hardened and ground locating surfaces |
| Application | indexing fixture for high mix electronics machining |
| Inspection | Dimensional report, material certificate, first article report on request |
| Lead time | 7–15 working days for samples, 3–4 weeks for production |
| Minimum order | 1 piece for prototypes, from 50 pieces for production pricing |
Manufacturing process
Production begins with a drawing and material review. Stock is certified, the operation sequence is fixed, and zero point clamping with modular workholding and tombstone fixtures is carried out on equipment maintained to hold repeatability within 0.005 mm over a full shift, not just on a first piece.
Material is purchased against a certificate and checked on receipt, so the composition is known before any cutting starts. Work in progress is identified by part number and operation, and the finished parts are deburred, cleaned and protected before they leave the machine area.
Typical applications
Most of the work supplied in this category falls into the following examples.
- Holding multiple small parts in one cycle.
- Machining five faces of a housing.
- Repeat batches on retained fixtures.
- Inspecting and re-loading without re-indicating.
- Heavy roughing with rigid clamping.
Quality control and documentation
Inspection is not a final formality. Dimensions are checked during the cycle and again at the end, so drift is corrected while there is still stock to remove.
Material certificates to EN 10204 3.1, dimensional reports and first article inspection reports are issued with the shipment where the application requires them. Calibration dates and measurement uncertainty are recorded alongside every result.
Ordering, lead time and packaging
Orders start from a single piece. Samples are quoted from the 3D model, and production pricing follows once quantity, finishing and inspection are agreed.
Frequently asked questions
How much setup time does zero point clamping save?
Changeovers typically fall from 45 minutes to under 5, because the part is located by the receiver rather than indicated on the table, and the next fixture is built while the machine runs.
Is the repeatability good enough for tight parts?
Quality systems repeat within about 0.005 mm, which is sufficient to remove and re-load a part mid-process without re-establishing datums.
How long does delivery take?
Sample parts are typically shipped in 7 to 15 working days after drawing approval. Production batches run 3 to 4 weeks depending on quantity, finishing and inspection requirements.
Send the drawing or the 3D model for a quotation. Include material, quantity, tolerance and finish, and a detailed quote with lead time is returned within one working day.