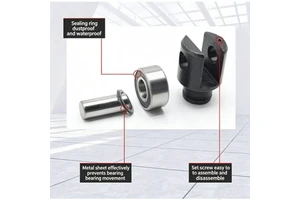
A Belt Conveyor System gets the same part to the same place in the same orientation, thousands of times without jamming. Supplied to fastener and hardware producers, this Belt Conveyor System is configured with a servo drive and programmable indexing. mechanical handling with guided part presentation and jam detection is carried out on equipment that holds ±0.2 mm across a full shift, not only on a first piece.
Tolerance is applied where it does work rather than across the whole drawing. Critical features are held to ±0.2 mm, non-critical dimensions follow the general machining tolerance, and the difference is stated in the quotation rather than discovered later.
Specification
| Process | Mechanical handling with guided part presentation and jam detection |
|---|---|
| Material / configuration | a servo drive and programmable indexing |
| Size / capacity | bar stock from 5 to 80 mm diameter |
| Tolerance | ±0.2 mm |
| Surface finish | stainless or anodised aluminium construction |
| Application | belt conveyor system for fastener and hardware producers |
| Inspection | Dimensional report, material certificate, first article report on request |
| Lead time | 7–15 working days for samples, 3–4 weeks for production |
| Minimum order | 1 piece for prototypes, from 50 pieces for production pricing |
Manufacturing process
Work is carried out with mechanical handling with guided part presentation and jam detection. Tooling, speeds and fixturing are recorded with the part number, so a repeat order starts from a proven process instead of a fresh setup.
Material is purchased against a certificate and checked on receipt, so the composition is known before any cutting starts. Work in progress is identified by part number and operation, and the finished parts are deburred, cleaned and protected before they leave the machine area.
Typical applications
Most of the work supplied in this category falls into the following examples.
- Presenting blanks to a press.
- Feeding bar stock to a lathe.
- Orienting small turned parts.
- Moving parts between machining operations.
- Accumulating finished parts for packing.
Quality control and documentation
Critical features are measured on calibrated equipment in a controlled room, and the results are filed with the job so that a repeat order can be compared with the first.
Material certificates to EN 10204 3.1, dimensional reports and first article inspection reports are issued with the shipment where the application requires them. Calibration dates and measurement uncertainty are recorded alongside every result.
Ordering, lead time and packaging
Packaging is specified by the part: individual protection for finished surfaces, separation for assemblies, and export crating with a packing list for shipment.
Frequently asked questions
Why does feeding fail more often than the machine it serves?
Because orientation is geometry dependent. Parts that nest or tangle need escapements, orientation features or vision, and that is designed from the part model rather than bought in.
Can one feeder handle several part numbers?
Yes, with quick change tooling or a flexible vision feeder. Dedicated bowl tooling is cheaper per part at volume, so the choice depends on mix and quantity.
Can you supply material and inspection certificates?
Yes. Material certificates to EN 10204 3.1, full dimensional reports, first article inspection reports and, where required, PPAP or AS9102 documentation are issued with the shipment.
Drawings are reviewed for manufacturability before quotation, and any feature that adds cost without adding function is pointed out at that stage rather than after the parts are made.