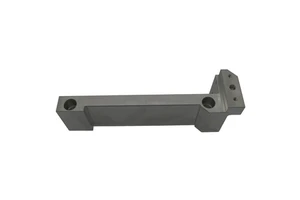
Mould Inserts in a production cell: cycle time and capacity
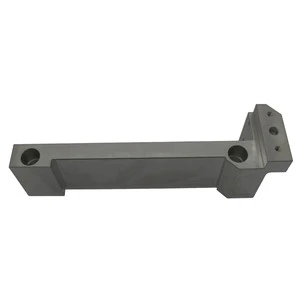
Mould Inserts is a replaceable steel component that forms part of a mould cavity. It is used for moulds where a wear area, a core or a detail needs to be replaced or machined separately. This entry explains what it is, what the numbers on a data sheet mean, and what to put on a drawing.
It is written from the point of view of the buyer and the drawing office: the values that are realistic in production, the ones that cost money, and the way the result is verified. Where an industry sets the requirement, aerospace is used as the example: traceability and a first article before anything enters the batch.
Cycle time
A realistic cycle for Mould Inserts is 4 to 20 hours per insert. That figure includes handling and measurement, not just the cutting, because the part has to be taken out, checked and put back.
Capacity planning
Capacity is planned on available hours, not on nominal hours: setup, maintenance and measurement all take a share. Where a batch repeats, the setup is amortised and the effective capacity rises sharply.
Bottlenecks
- The detail and the finishing requirement, which is the usual limit on a single machine.
- Inspection, which queues when a batch is released at the end of a shift.
- Material availability, because H13 tool steel has to be on the bar before the machine can start.
| Item | Note |
|---|---|
| Cycle | 4 to 20 hours per insert |
| Cost driver | the detail and the finishing requirement |
| Tolerance | ±0.01 mm |
| Material | H13 tool steel |
| Documentation | in-house approval with dimensional reports |
Applications
Mould Inserts is used for moulds where a wear area, a core or a detail needs to be replaced or machined separately, and in practice it appears most often in injection moulds, die casting tools, blow moulds, prototype tooling.
How it fits into a machining route
Mould Inserts is produced by whichever route reaches it most reliably, and it is usually the reason the rest of the part is dimensioned the way it is. Datums are chosen so that this feature is measured from what it actually has to be square or concentric with.The route is fixed before the first part is cut, and it is the route rather than the individual setting that holds the result: the detail and the finishing requirement. Where a drawing calls for something the route cannot hold economically, that is raised at quotation rather than after the parts are made.
Standards, documentation and what is issued
The documentation requirement is in-house approval with dimensional reports. Material is supplied against a certificate where the application calls for it, inspection results are recorded with the job, and the records are kept so that a repeat order can be compared with the first instead of being measured from scratch.
CMM for the form, and a fit check in the bolster is the verification step. Where a customer format or a standard report is required, it is agreed before the batch starts, because a report written after the event is a report nobody can use.
Frequently asked questions
What tolerance should be specified for Mould Inserts?
±0.01 mm is realistic in production. Tightening it beyond the functional requirement increases cost without improving the part.
Which material is usually used?
H13 tool steel is the usual choice, supplied against in-house approval with dimensional reports.
How is the result verified?
CMM for the form, and a fit check in the bolster, with the results recorded so a repeat order can be compared with the first.
What is the most common mistake?
A shut off face that is not square, which flashes.
How long does it take and what does it cost?
A realistic cycle is 4 to 20 hours per insert, and the cost driver is the detail and the finishing requirement.
Related capability
If you are specifying Mould Inserts on a drawing and want a second opinion on the route, send the model and the quantity. The first response is a manufacturability review with the likely risk points and a quotation, so the decision can be made on facts rather than on a price alone.
Machining, inspection and documentation are handled in one place, which is why the dimensional report and the material certificate arrive with the parts rather than after them.
Related entries
These entries sit next to Mould Inserts in the encyclopedia: Hydraulic Manifolds, Heat Sinks, Geometric Dimensioning and Tolerancing. Reading them together gives a fuller picture of how the process, the material and the measurement affect each other.



