Horizontal Machining Centre in a production cell: cycle time and capacity
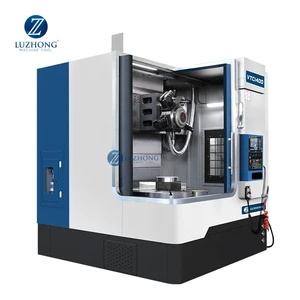
Horizontal Machining Centre is a milling machine with a horizontal spindle and a rotary table, usually with pallet exchange. It is used for parts that need work on several faces in one setup, and for unattended running. This entry explains what it is, what the numbers on a data sheet mean, and what to put on a drawing.
It is written from the point of view of the buyer and the drawing office: the values that are realistic in production, the ones that cost money, and the way the result is verified. Where an industry sets the requirement, automotive is used as the example: a fixed takt, because a late delivery stops the line.
Cycle time
A realistic cycle for Horizontal Machining Centre is 20 to 60 minutes per pallet. That figure includes handling and measurement, not just the cutting, because the part has to be taken out, checked and put back.
Capacity planning
Capacity is planned on available hours, not on nominal hours: setup, maintenance and measurement all take a share. Where a batch repeats, the setup is amortised and the effective capacity rises sharply.
Bottlenecks
- Pallet utilisation, because an idle pallet is still a cost, which is the usual limit on a single machine.
- Inspection, which queues when a batch is released at the end of a shift.
- Material availability, because 316L stainless steel has to be on the bar before the machine can start.
| Item | Note |
|---|---|
| Cycle | 20 to 60 minutes per pallet |
| Cost driver | pallet utilisation, because an idle pallet is still a cost |
| Tolerance | ±0.01 mm |
| Material | 316L stainless steel |
| Documentation | AS9100 or IATF 16949 depending on the customer |
Applications
Horizontal Machining Centre is used for parts that need work on several faces in one setup, and for unattended running, and in practice it appears most often in gearbox housings, pump bodies, valve bodies, structural aerospace parts.
How it fits into a machining route
Horizontal Machining Centre is one station in a route rather than the whole of it. The part arrives with the previous operation finished and leaves with the features it is responsible for completed, so the datum and the clamping method are agreed before the first part rather than discovered on it.The route is fixed before the first part is cut, and it is the route rather than the individual setting that holds the result: pallet utilisation, because an idle pallet is still a cost. Where a drawing calls for something the route cannot hold economically, that is raised at quotation rather than after the parts are made.
Standards, documentation and what is issued
The documentation requirement is AS9100 or IATF 16949 depending on the customer. Material is supplied against a certificate where the application calls for it, inspection results are recorded with the job, and the records are kept so that a repeat order can be compared with the first instead of being measured from scratch.
CMM with the part on its locating features is the verification step. Where a customer format or a standard report is required, it is agreed before the batch starts, because a report written after the event is a report nobody can use.
Frequently asked questions
What tolerance should be specified for Horizontal Machining Centre?
±0.01 mm is realistic in production. Tightening it beyond the functional requirement increases cost without improving the part.
Which material is usually used?
316L stainless steel is the usual choice, supplied against AS9100 or IATF 16949 depending on the customer.
How is the result verified?
CMM with the part on its locating features, with the results recorded so a repeat order can be compared with the first.
What is the most common mistake?
The rotary axis not checked for backlash before a batch starts.
How long does it take and what does it cost?
A realistic cycle is 20 to 60 minutes per pallet, and the cost driver is pallet utilisation, because an idle pallet is still a cost.
Related capability
If you are specifying Horizontal Machining Centre on a drawing and want a second opinion on the route, send the model and the quantity. The first response is a manufacturability review with the likely risk points and a quotation, so the decision can be made on facts rather than on a price alone.
Machining, inspection and documentation are handled in one place, which is why the dimensional report and the material certificate arrive with the parts rather than after them.
Related entries
These entries sit next to Horizontal Machining Centre in the encyclopedia: Coordinate Measuring Machine, CNC Drilling Machine, CNC Turning. Reading them together gives a fuller picture of how the process, the material and the measurement affect each other.



