Hard Machining and EDM Programme for Aerospace Actuator Housings
A hard machining and edm programme is not a quotation for a part number. It is an agreement about how actuator housings will be made, measured and released every time they are ordered. This page sets out what that looks like for actuator housings in Ti-6Al-4V titanium, where the difficulty is weight targets that leave almost no margin for oversized sections.
The work described here runs in a route combining hard milling, wire EDM and grinding for Aerospace customers. The buyer signs off the first article before anything enters the batch, and parts that carry load and cannot be reworked once the assembly is closed. The route below is the one we would propose on a first enquiry, and it is the one we would still be running two years later.
What this programme has to deliver
These are the four things that decide whether a hard machining and edm programme works in practice. Everything else is detail that gets settled at the quotation stage.
- Dimensions held to ±0.01 mm on the features that locate the part, not just on the ones that are easy to measure.
- Material supplied against a certificate, because AS9100 with full material traceability applies to this work.
- Repeatability between batches, so the hundredth part assembles like the first.
- Documentation that arrives with the parts rather than two weeks after they do.
Process route
The route is hard milling and wire EDM after heat treatment. Operation order is fixed before the first part is cut: roughing to leave even stock, stress relieving where the geometry needs it, semi finishing, then the finishing operations that hold ±0.01 mm. That order is what keeps the tolerance stable as the machine warms up and the batch runs.
| Programme | Hard Machining and EDM Programme |
|---|---|
| Typical parts | actuator housings |
| Material | Ti-6Al-4V titanium |
| Tolerance | ±0.01 mm on locating features |
| Batch size | 5 to 200 pieces |
| First parts | 10 to 20 working days |
| Equipment | a route combining hard milling, wire EDM and grinding |
| Documentation | AS9100 with full material traceability |
The advantage of running it this way is that the part is finished after hardening, so heat treatment distortion is removed from the tolerance chain. Where a drawing calls for something the route cannot hold economically, that is raised at quotation rather than after the parts are made.
Materials, tolerances and finishes
Ti-6Al-4V titanium is purchased against a certificate and checked on receipt, so the composition is known before any cutting starts. Where the application calls for a different grade, the change is quoted with the machining implications spelled out rather than absorbed silently.
±0.01 mm is held on the features that matter and left open elsewhere, because a tolerance that costs money without adding function is a cost the drawing should not carry. Surface finish, edge breaks and protective treatments are specified on the drawing and confirmed before packing.
Typical parts in this programme
The part numbers that come through this route tend to look alike in the way that matters: they are parts that carry load and cannot be reworked once the assembly is closed. A representative list for Aerospace work looks like this.
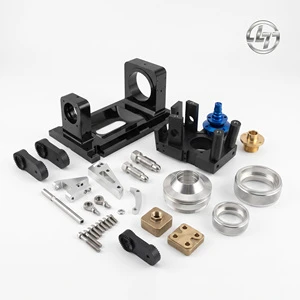
- Structural Brackets in Ti-6Al-4V titanium, machined complete in as few setups as the geometry allows.
- Wing rib fittings where the tolerance stack up is carried by the machining rather than by the assembly.
- Actuator housings that repeat on a known cycle, usually released against a schedule rather than one order at a time.
- Revision work on the same family, where a drawing change has to be absorbed without a new fixture.
In each case the quotation is built on the route rather than on a single part number, which is why the price holds when the batch is repeated and the design moves on.
What drives the cost
Four things move the number, and they are worth separating because they are usually confused with each other. Tolerance is the first: holding ±0.01 mm across a batch costs more than holding it once, because it has to be measured and because the tooling has to be managed. Material is the second, and Ti-6Al-4V titanium is priced on the certificate as well as on the bar.
Batch size is the third. Setups and first article inspection are fixed costs, so 5 to 200 pieces spreads them differently depending on how the order is released. Surface treatment and packing are the fourth, and they are quoted separately so that a change of finish does not force a re-quote of the machining.
Quality assurance and documentation
Critical features are measured on calibrated equipment in a controlled room and the results are filed with the job, so a repeat order can be compared with the first instead of being measured from scratch.
AS9100 with full material traceability. Calibration dates and measurement uncertainty are recorded with every result, and first article reports are issued where the application requires them.
How a programme starts
Three steps, and none of them commit anyone to a production order. First, the drawing and model are reviewed for manufacturability, and anything that adds cost without adding function is pointed out at that stage. Second, a quotation is issued with the route, the batch assumption and the lead time written into it.
Third, the first parts are made, measured and reported. That report is the basis for release: if the dimensions and the documentation are accepted, the route is fixed and the programme runs on a schedule. If something needs changing, it is changed before the batch starts rather than during it.
Programme timing, capacity and logistics
First parts are quoted at 10 to 20 working days and production runs at 5 to 200 pieces. Capacity is held against a schedule rather than promised in the abstract, and call off quantities are agreed so that material is available when the order releases.
Packaging is specified by the part: individual protection for finished surfaces, separation for assemblies, and export crating with a packing list. Shipments leave with the documentation that matches the order.
Frequently asked questions
What do you need to quote actuator housings?
STEP or IGES for the model and a PDF drawing with tolerances, material and finish called out. Quantity and expected repeat frequency matter as much as the geometry, because they decide the route.
Can you hold ±0.01 mm in production, not just on the first article?
Yes. It is held by the process route and tool compensation rather than by sorting at inspection, which is why the operation order and the fixture are settled before the batch starts.
How is documentation handled?
AS9100 with full material traceability is issued with the shipment where the application requires it, and the records are kept with the job so that a later order can be traced back to the material batch and the measurement equipment used.
Can you work to our drawings and our standards?
Yes. Most of this work is made to customer drawings under the customer's own quality requirements. Where a standard conflicts with the drawing, the conflict is raised before quotation rather than resolved silently on the machine.
What happens if the drawing is still changing?
That is what the hard machining and edm programme is for. Changes are quoted on the delta rather than on a fresh part number, and the revision history is kept with the job.
Getting started
Send the drawing and the expected quantities. The first response is a manufacturability review with the route, the likely risk points and a quotation, so the decision can be made on facts rather than on a price alone.



