-
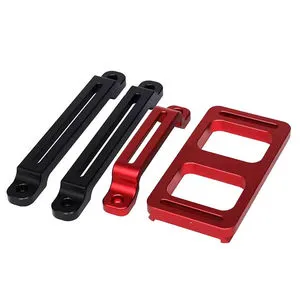
Batch Repeatability: 5 Units of Brake Caliper Mounting Bracket to One Standard
How we held consistent results across a 5-unit batch of a high-strength aluminium bracket for a performance braking system: the controls on tooling, offsets and inspection that keep the first part and the last part the same.
Details -
Cycle Time Down by 25 per cent: Machining Brake Caliper Mounting Bracket
A machining improvement programme on a high-strength aluminium bracket for a performance braking system: where the time was going, what we changed in roughing, tooling and handling, and the 25 per cent saving achieved without touching the.
Details -
Re-sourcing Brake Caliper Mounting Bracket: Taking Over an Existing Programme
How we took over an established programme for a high-strength aluminium bracket for a performance braking system: reviewing inherited drawings and samples, rebuilding the process, proving it and shipping the first approved batch.
Details -
Fixture Strategy for Brake Caliper Mounting Bracket: How We Held the Part
The fixture strategy behind a high-strength aluminium bracket for a performance braking system: how we located the part on its drawing datums, what was built, why those decisions were taken and how the setup performed in production.
Details -
Documentation Pack for Aluminium Busbar Connector: What Shipped with the Order
The documentation supplied with a shipment of a machined connector carrying currents above 300 A: what each document is for, why it matters at goods-in and how it is kept valid for repeat orders.
Details -
Emergency Rework: Recovering a Aluminium Busbar Connector Order Against the Clock
An emergency recovery job involving a machined connector carrying currents above 300 A: what went wrong at another source, how we planned the recovery in parallel, and how usable parts reached the customer line in time.
Details -
Scheduled Repeat Supply of Aluminium Busbar Connector: Planning, Stock and Kanban
A scheduled supply programme for a machined connector carrying currents above 300 A: how releases were agreed, how stock and tooling were held, and how forecast changes were handled without disruption.
Details -
Assembly Fit Check for Aluminium Busbar Connector: Machining to the Mating Part
Machining a machined connector carrying currents above 300 A against its mating part: how the fit was defined, checked on the shop floor and then verified at the customer's assembly line.
Details -
Material Change for Aluminium Busbar Connector: Trial, Validation and Approval
A material change programme for a machined connector carrying currents above 300 A: why the change was needed, how the trial part was machined and tested, and how the new material was validated and approved.
Details -
Design Feedback on Aluminium Busbar Connector: Changes Proposed Before Cutting
A design-for-manufacture review of a machined connector carrying currents above 300 A: the features that were expensive to produce, the changes we proposed, and how the function was preserved while simplifying the process.
Details -
Cycle Time Down by 25 per cent: Machining Aluminium Busbar Connector
A machining improvement programme on a machined connector carrying currents above 300 A: where the time was going, what we changed in roughing, tooling and handling, and the 25 per cent saving achieved without touching the drawing.
Details -
Batch Repeatability: 5 Units of Aluminium Busbar Connector to One Standard
How we held consistent results across a 5-unit batch of a machined connector carrying currents above 300 A: the controls on tooling, offsets and inspection that keep the first part and the last part the same.
Details
Case Studies